Automation controls for industrial equipment from architecture to secure operation
What automation controls mean in industrial equipment
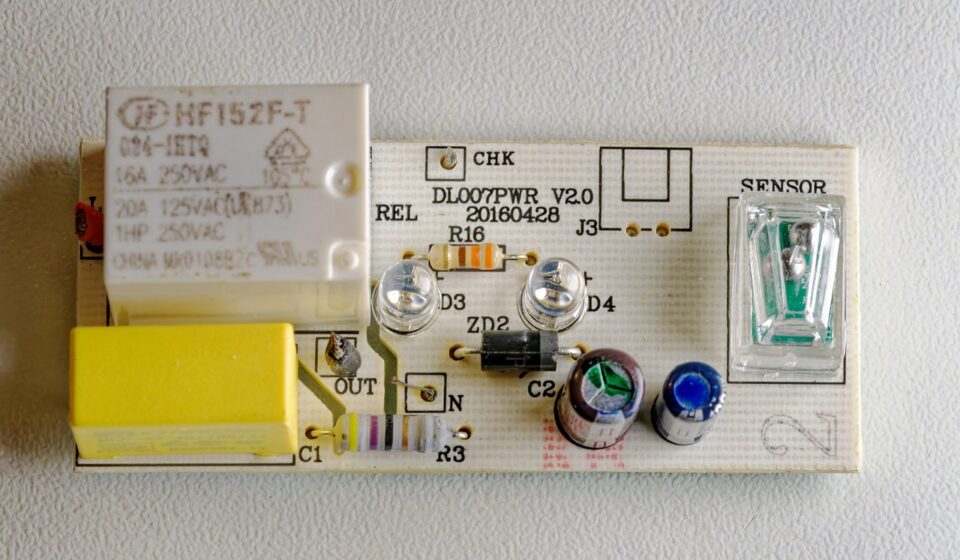
Automation controls are the hardware, software, networks, logic, and operating practices used to monitor equipment conditions and direct machine or process behavior. In industrial equipment, the automation controls stack typically extends from sensors and input/output modules to PLCs, drives, motion controllers, safety circuits, HMIs, SCADA systems, and data interfaces.
The purpose is not simply to replace manual work. A well-designed control system makes operation repeatable, reduces avoidable downtime, supports safe intervention, and gives maintenance teams enough diagnostic information to act before small issues become production losses.
For equipment owners and system integrators, the practical question is not whether a system should be automated. It is which decisions should be made locally in the machine, which decisions should remain visible to operators, which functions require independent safety controls, and which data should be shared with higher-level systems.
The control loop from sensor to action
Most automation controls follow a repeating loop: measure, decide, act, and verify. A temperature transmitter measures a process variable, a controller compares that value with a setpoint, an output signal adjusts a valve or heater, and the next measurement confirms whether the action moved the process in the right direction. The same pattern appears in speed control, pressure regulation, level control, robotic positioning, and packaging line sequencing.
Sensing and measurement
Sensors and instruments determine the quality of the control decision. A controller cannot reliably compensate for a poorly located proximity sensor, an incorrectly ranged pressure transmitter, or a noisy encoder signal without adding complexity and risk. Selection should account for accuracy, response time, environmental rating, calibration needs, failure mode, and how the signal will be diagnosed when it drifts or fails.
Control logic
The logic layer usually runs in a PLC, PAC, motion controller, DCS controller, or embedded industrial controller. It handles sequencing, interlocks, setpoint management, alarms, permissives, recipe changes, and recovery states. Good logic is explicit about what the machine should do during startup, normal production, cleaning, product changeover, power loss, emergency stop, and restart after fault clearance.
Actuation and supervision
Actuators turn control decisions into physical movement or process change. They include contactors, solenoids, valves, variable frequency drives, servo drives, heaters, pumps, and robots. HMIs and SCADA systems make status, alarms, trends, and operator actions visible. These supervisory systems are important, but they should not be the only place where critical control behavior is defined.
Core components and selection questions
| Component | Main role | Selection questions |
|---|---|---|
| Sensors and instruments | Measure position, pressure, flow, temperature, speed, level, vibration, or product presence | Is the signal accurate, fast, serviceable, and suitable for the environment? |
| I/O modules | Connect field devices to controllers | Are channel count, isolation, diagnostics, spare capacity, and wiring method adequate? |
| PLC, PAC, or controller | Execute deterministic logic and machine sequencing | Can it meet scan time, memory, communication, safety, and support requirements? |
| Drives and motion | Control speed, torque, position, and energy use | Are load profile, braking, feedback, tuning, and safety functions understood? |
| HMI and SCADA | Provide operator interface, alarms, trends, and supervisory visibility | Are screens usable under abnormal conditions, not only during normal production? |
| Safety controller or relay | Execute defined safety functions independently from standard control | Has the required performance level or safety integrity level been determined? |
| Industrial network | Move control and diagnostic data between devices and systems | Are latency, segmentation, protocol support, redundancy, and security controls defined? |
This table shows why automation controls should be specified as a system, not as a parts list. A fast controller with weak diagnostics, a sophisticated HMI with unclear alarm priorities, or a highly networked device without a maintenance plan can all create operational problems.
Standards and guidance that shape control design
Several widely used standards and guidance documents influence industrial automation controls. They do not replace engineering judgment, but they help teams use common language and avoid preventable design gaps.
IEC 61131-3:2025, published on May 22, 2025, is the current IEC edition covering programming languages for programmable controllers. IEC describes it as specifying syntax and semantics for languages such as structured text, ladder diagram, and function block diagram, while sequential function chart is used to structure the internal organization of programs and function blocks. For equipment teams, the value is not only language preference. The standard also supports maintainable logic, consistent documentation, and long-term support across vendors and facilities.
ISO 13849-1:2023 addresses safety-related parts of control systems for machinery, including design and integration principles. IEC 62061:2021 addresses functional safety of safety-related control systems for machines and sits within the broader IEC 61508 framework. IEC also lists amendments to IEC 62061 in 2024 and 2026, so project teams should verify the edition required by the customer, machine type, and jurisdiction before freezing specifications.
In the United States, OSHA 29 CFR 1910.147 covers the control of hazardous energy during servicing and maintenance where unexpected energization, startup, or stored energy release could injure employees. This distinction matters in control design: a software stop, HMI command, or normal interlock is not the same as verified hazardous energy isolation for maintenance. Safety design, operating controls, and lockout/tagout procedures should be treated as related but separate layers.
PLC, DCS, SCADA, and edge control are not interchangeable
Many project delays start when architecture choices are made by brand familiarity rather than by function. PLCs and PACs are commonly used for discrete machines, packaging lines, material handling, utility skids, and high-speed equipment sequencing. They are well suited to deterministic I/O handling and local machine control.
DCS platforms are more common in continuous and batch process environments where many control loops, operator stations, alarm strategies, historian connections, and process units must be coordinated. SCADA systems are often used for supervisory control and data acquisition across lines, sites, utilities, and geographically distributed assets. They provide visibility and coordination, but the fastest and most critical closed-loop decisions should usually remain local to the controller or safety system.
Edge gateways and industrial computers can add protocol translation, buffering, analytics, and data routing. They should be introduced with clear boundaries. If an edge device fails, the machine should degrade in a defined way rather than losing basic control. This is especially important when cloud dashboards, remote service, or enterprise reporting are added to equipment that must continue operating safely.
Cybersecurity is now part of automation controls selection
Modern automation controls are rarely isolated. Remote support, plant networks, historians, quality systems, energy monitoring, and vendor tools all increase the number of connections around a control system. NIST SP 800-82 Rev. 3, finalized on September 28, 2023, describes operational technology as programmable systems and devices that interact with the physical environment and emphasizes that OT security must respect performance, reliability, and safety requirements. NIST also began work on SP 800-82 Rev. 4 with a January 22, 2026 pre-draft call for comments, with the comment period closing on February 23, 2026. As of September 5, 2026, teams should treat Rev. 3 as final guidance while monitoring Rev. 4 development.
The ISA/IEC 62443 series focuses specifically on industrial automation and control systems cybersecurity across the lifecycle. ISA announced ANSI/ISA-62443-2-1-2024 on January 28, 2025, covering security program requirements for IACS asset owners. The practical lesson is that cybersecurity should be designed into equipment procurement, system integration, commissioning, maintenance, and supplier access rather than added after factory acceptance testing.
Useful cybersecurity questions include: who can change logic, how remote access is approved, whether controller backups are tested, how firmware and patches are evaluated, which assets are inside each network zone, and how abnormal traffic or unauthorized changes are detected. Strong automation controls depend on recoverability as much as prevention.
A practical workflow for selecting automation controls
- Define the process and failure modes. Document normal operation, startup, shutdown, cleaning, maintenance, product changeover, jams, power loss, air loss, and restart conditions.
- Separate standard control from safety functions. Standard logic can improve production, but safety functions need their own risk assessment, architecture, validation, and documentation.
- Size the system with margin. Include spare I/O, panel space, processor capacity, network ports, memory, and power supply headroom for realistic future changes.
- Choose platforms that can be supported. Availability of spares, programming tools, trained technicians, documentation, and vendor lifecycle information can matter more than a small difference in hardware cost.
- Verify communication needs. OPC UA is widely used for structured industrial data exchange, while MQTT is an OASIS standard publish/subscribe transport often used in machine-to-machine and IoT contexts. The right choice depends on data model, latency, bandwidth, ownership, and security requirements.
- Plan commissioning and recovery. Define software version control, backup storage, restore testing, alarm review, acceptance tests, and post-startup tuning before the equipment ships.
This workflow adds information that is often missing from simple component comparisons. The real cost of automation controls is determined over the equipment lifecycle, not only at purchase order approval.
Common mistakes that reduce reliability
- Designing only for normal production. Machines often fail during transitions, restarts, cleaning, and manual intervention.
- Treating alarms as messages instead of priorities. Operators need actionable alarms, not a flood of equal-severity notifications.
- Using safety devices as production sensors. Safety functions should not be compromised to solve ordinary sequencing problems.
- Adding cybersecurity after networking decisions. Segmentation, user roles, backups, and remote access rules should be defined before commissioning.
- Relying on undocumented tribal knowledge. If technicians cannot understand the logic, fault handling, and bypass conditions, downtime and unsafe workarounds become more likely.
The better approach is to document intent: what the equipment should do, why it should do it, what should never happen, and how operators and maintenance teams can verify the state of the system.
Frequently asked questions
Are automation controls the same as industrial automation?
No. Industrial automation is the broader activity of automating machines, processes, lines, and plants. Automation controls are the control-system layer that makes automated behavior possible, including sensing, logic, actuation, safety, operator interface, and communication.
What is the difference between a PLC and SCADA?
A PLC executes local control logic and directly handles I/O, sequencing, and interlocks. SCADA provides supervisory visibility, alarms, trends, and coordination across equipment or sites. SCADA can send commands, but the most time-critical equipment behavior should normally remain in the controller.
Can an HMI stop button replace lockout/tagout?
No. An HMI command or software stop may be part of normal operation, but hazardous energy control for servicing and maintenance requires defined isolation, lockout or tagout procedures, and verification according to applicable rules. In U.S. general industry, OSHA 29 CFR 1910.147 is the key reference.
Which standards should be checked first?
Start with the machine type, location, risk level, and customer requirements. Common references include IEC 61131-3 for programmable controller languages, ISO 13849-1 and IEC 62061 for machinery safety-related control systems, ISA/IEC 62443 for IACS cybersecurity, and NIST SP 800-82 for OT security guidance.
How much data should automation controls send to higher-level systems?
Send data that supports operation, maintenance, quality, energy review, and compliance. Avoid exporting every raw signal without a purpose. More data can increase storage, bandwidth, cybersecurity exposure, and alarm noise if the architecture and ownership model are unclear.
Source note: This article summarizes publicly available information from NIST SP 800-82 Rev. 3 and Rev. 4 pre-draft materials, ISA/IEC 62443 publications, IEC 61131-3:2025, ISO 13849-1:2023, IEC 62061:2021, OSHA 29 CFR 1910.147, OPC Foundation materials, and OASIS MQTT materials.