How to choose a material handling conveyor for industrial flow
What a material handling conveyor should solve
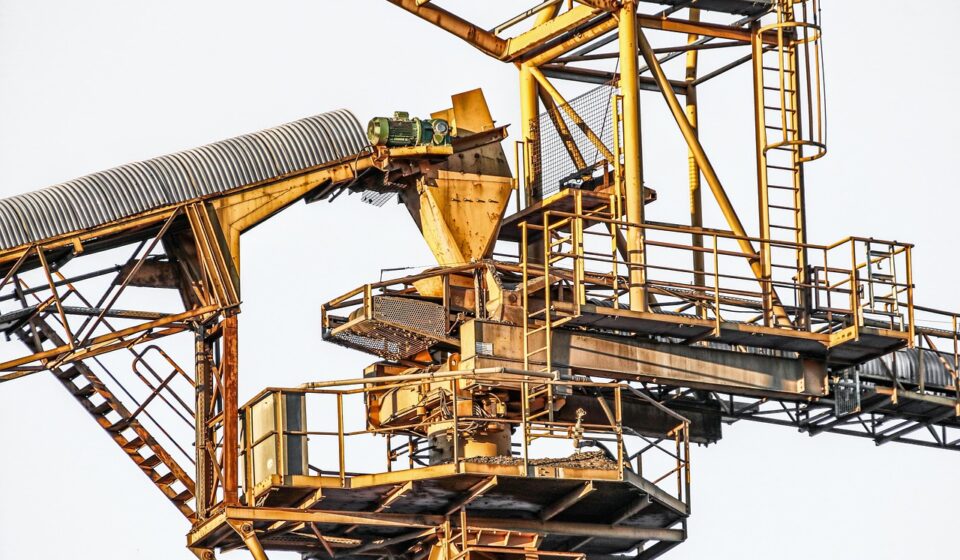
A material handling conveyor is a fixed or semi-fixed system that moves materials, products or loads through a manufacturing, warehousing or distribution process. The right choice is not simply the fastest belt or the longest line. It is the conveyor that fits the site’s load, route, speed, safety requirements, controls and maintenance capability.
For an industrial facility, the better starting question is: where is the flow constraint? A conveyor should reduce non-value-added travel, stabilize handoffs between processes and make movement more predictable. If it only moves the bottleneck from picking to packing, receiving to storage, or production to palletizing, the project has not solved the real material flow problem.
This guide reviews the main conveyor types, the specification choices that affect performance, and the safety and maintenance factors that should be checked before a purchase decision.
What conveyors do inside material flow
Industry guidance from MHI describes conveyors as equipment used to move materials, products and loads throughout a facility in horizontal, inclined or vertical directions. In practice, they create a controlled path between points that repeatedly exchange goods, such as receiving and inspection, storage and picking, machining and assembly, packaging and shipping, or processing and bulk discharge.
The operational value is repeatability. A forklift route depends on traffic, driver availability and aisle access. A conveyor route is easier to pace, monitor and connect to upstream or downstream equipment. This is why conveyors are common in e-commerce, food, beverage, automotive, pharmaceuticals, paper, plastics, manufacturing and warehousing.
The same principle applies across these sectors: when material moves often, in known directions, and with enough volume to justify fixed equipment, a conveyor can reduce manual travel and make production or fulfillment rhythm more consistent.
Main conveyor types and common applications
Many selection problems start when a facility chooses by equipment name instead of load behavior. The table below summarizes common conveyor options and the situations where they usually fit.
| Conveyor type | Typical loads | Best fit | Key limitation |
|---|---|---|---|
| Belt conveyor | Cartons, parcels, bags, small parts | Continuous movement, inclines and general transport | Belt tracking, cleaning and wear must be managed |
| Roller conveyor | Totes, cartons and pallets with stable bottoms | Accumulation, staging and medium-duty transfers | Irregular or soft-bottom loads may not travel reliably |
| Chain conveyor | Pallets, skids and heavy unit loads | Heavy-duty transport and transfer between pallet processes | Not ideal for light cartons or fragile products |
| Screw conveyor | Powders, grains, chips and bulk solids | Enclosed bulk movement, metering and process feeding | Material degradation and cleaning access require review |
| Vertical conveyor or lift | Totes, cartons, pallets or carriers | Moving loads between floors or mezzanine levels | Throughput depends on cycle time and loading method |
| Sortation conveyor | Parcels, cartons and totes | Routing products to lanes, zones or destinations | Needs accurate identification, spacing and controls |
CEMA standards and technical publications separate conveyor categories because each design has different terminology, dimensional expectations, guarding concerns and application limits. A belt conveyor that performs well in carton transport may be a poor choice for abrasive bulk material. A gravity roller line that works in a packing cell may fail if the product base is flexible, wet or inconsistent.
Selection criteria that matter before layout is frozen
Load profile
The load profile is the foundation of the specification. A buyer should document minimum and maximum size, weight, base condition, center of gravity, fragility, temperature, moisture, dust, contamination risk and packaging variation. For bulk materials, density, particle size, abrasiveness, flowability and cleaning requirements become more important than carton dimensions.
For unit loads, the surface that touches the conveyor is critical. A tote with a rigid flat bottom behaves differently from a bag, pail, tire or shrink-wrapped bundle. Small differences in the load base can change roller spacing, belt selection, transfer design and accumulation method.
Route and handoff points
Conveyors do not operate in isolation. They interface with dock equipment, storage systems, machines, robots, sorters, palletizers, inspection stations and human work areas. Each transfer point should be reviewed for product orientation, drop height, side pressure, accumulation, jam recovery and operator access. Many reliability problems begin at transitions rather than on the straight conveyor section.
Throughput and accumulation
Throughput should be specified as a realistic range, not only as a peak target. The design team should define average units per hour, peak units per hour, peak duration, required spacing, batch changes and downtime assumptions. Accumulation zones may be needed where upstream and downstream processes run at different rates.
Zero pressure accumulation can reduce product contact, while simpler accumulation may be acceptable for robust loads. The right answer depends on product damage tolerance and process rhythm.
Controls and data
Modern conveyor decisions often involve sensors, drives, PLCs, scanners, weighers, diverters and warehouse or production software. A basic transport conveyor may need only start-stop control and emergency stops. A sortation or automated storage interface needs tracking logic, fault reporting and communication with a WMS, WCS or production control system.
Controls should be planned early because mechanical layout, spacing and accumulation logic all affect data accuracy. If identification points, divert spacing or accumulation zones are added late, the mechanical design may need to change. See also: automation and controls.
Safety, standards and maintainability should shape design
Conveyor safety should be designed into the system rather than added after installation. Public U.S. references commonly relevant to conveyor environments include OSHA rules for general machine guarding, control of hazardous energy, walking-working surfaces, and materials handling and storage. OSHA warehousing guidance also emphasizes guarding, safe work surfaces, lighting, inspection and conveyor safety mechanisms. These references do not replace a site-specific compliance review, but they show the areas industrial buyers should not leave vague.
CEMA publishes conveyor standards, terminology resources and safety best-practice material covering topics such as emergency-stop application, spill guarding, supplemental guarding and conveyor crossovers. In a specification, these references help convert broad safety language into concrete design questions: Where are nip points? How will maintenance lockout be performed? Can personnel cross safely? Are emergency stops reachable? Are guards removable only with tools where required? Is jam clearing considered a normal task or an exceptional maintenance activity?
The broader safety context matters. In its 2024 warehousing and storage industry data, the U.S. Bureau of Labor Statistics reported a total recordable injury and illness rate of 4.8 cases per 100 full-time workers and 32 fatalities in NAICS 493. Those figures are not conveyor-specific, but they underline why material movement equipment should be evaluated for risk exposure as well as capacity.
Maintainability is part of the same decision. A conveyor that is difficult to clean, inspect, lubricate, align or isolate will lose availability over time. Buyers should ask about belt access, roller replacement, spare-part lead times, motor and drive standardization, lubrication intervals, cleaning methods, guarding removal, sensor access and diagnostic visibility.
Conveyor, mobile automation or manual handling
A material handling conveyor is strongest when the path is stable, volume is repeatable and the handoff points are known. Mobile robots, forklifts and carts are stronger when routes change frequently, volumes are still uncertain or the operation needs flexible point-to-point movement. Manual handling remains useful for low-volume, highly variable or delicate work, but it should not be used to hide a flow problem that can be engineered out.
The choice is often hybrid. A facility may use conveyors for high-volume trunk lines, mobile robots for flexible replenishment, lifts for level changes and manual stations for exception handling. The design goal is not maximum automation. It is the right movement method for each segment of the process.
A practical conveyor specification checklist
- Define the product or material range, including worst-case size, weight and surface condition.
- Map every origin, destination, merge, divert, lift and transfer point.
- Separate average throughput from peak throughput and define peak duration.
- Identify where accumulation is required and what product contact is acceptable.
- Confirm cleaning, dust, moisture, temperature and contamination constraints.
- Review guarding, emergency stops, lockout points, crossovers and maintenance access before approval.
- Specify control interfaces, scanners, sensors and data reporting needs early.
- Ask which standards, safety practices and acceptance tests will be used.
- Plan spare parts, preventive maintenance and operator training before go-live.
The strongest conveyor projects are usually the clearest ones. When the load, flow path, controls and safety expectations are documented early, suppliers can compare real requirements rather than guessing at intent. That reduces redesign, improves commissioning and makes the conveyor a durable part of industrial material flow.
Frequently asked questions
What is the difference between a conveyor and a sorter?
A conveyor primarily moves loads from one point to another. A sorter identifies, separates or routes items to different destinations. Many automated systems combine both functions, but control complexity and spacing requirements increase when sorting is involved.
When is a belt conveyor better than a roller conveyor?
A belt conveyor is often better for small, irregular, soft-bottom or inclined loads. A roller conveyor is often better for cartons, totes or pallets with stable bases, especially where accumulation or staging is needed.
What information should be sent to a conveyor supplier first?
Start with load dimensions and weight, product photos, current process map, desired throughput, facility layout, elevation changes, available utilities, safety requirements, cleaning needs and software interfaces. This information is more useful than asking for a generic conveyor price.
Can a conveyor improve safety?
It can reduce manual carrying and travel, but only if it is designed with proper guarding, access, emergency stops, lockout provisions and training. A poorly guarded or hard-to-maintain conveyor can introduce new hazards, so safety must be part of the specification from the beginning.