Floor mounted pallet flow explained for FIFO staging and case picking
What floor mounted pallet flow is
Floor mounted pallet flow is a floor-level material handling layout that uses roller tracks, wheel beds, rails, or low support structures to move pallets through defined lanes. In most applications, it supports first-in, first-out inventory rotation, dock staging, production line feeding, or case-pick replenishment without requiring a full-height pallet flow rack.
The main value is controlled movement, not storage density alone. Pallets enter from one side, advance through a lane, and are retrieved from the opposite side or from a clearly defined pick face. That makes the system useful where inventory must remain visible, accessible, and sequenced at ground level.
For warehouse and plant teams reviewing material flow options, floor mounted lanes sit between basic floor stacking and elevated pallet flow racking. They can reduce random staging, improve rotation discipline, and create a more predictable interface between forklifts, pallet jacks, conveyors, and manual picking zones.
How it differs from standard pallet flow rack
Standard pallet flow rack is normally installed within a rack structure. Pallets are loaded at the higher end and move by gravity toward a lower pick face. MHI educational material describes pallet flow as a system that uses conveyor wheel shelf sections to let back-loaded pallets move toward the front or pick face, typically supporting FIFO inventory control. Floor mounted pallet flow uses a similar movement principle, but the lanes are placed at or near floor level rather than on elevated rack beams.
This difference changes how the system is used. Rack-based pallet flow is often selected for high-density storage across multiple vertical levels. A floor mounted version is more often selected for staging, replenishment, assembly support, dock buffers, freezer or cooler picking zones, or any area where the first pallet position needs to remain accessible without lifting to a rack level.
The distinction also matters for risk review. A full rack structure introduces rack design, anchoring, beam capacity, upright protection, seismic considerations, and elevated-load hazards. Floor mounted lanes may reduce some vertical rack concerns, but they still require engineering attention for load weight, lane pitch, pallet condition, braking, guarding, traffic separation, and floor condition.
Common operating patterns
Floor mounted pallet flow is not a single design. The term is used across several related layouts, each with different operating limits.
Gravity-fed FIFO lanes
In a gravity-fed lane, pallets are loaded from the rear or high side and move forward along wheel or roller tracks. This layout is closest to conventional pallet flow rack. It works best when pallet size, pallet quality, and load weight are reasonably consistent. The lane must be pitched and controlled so pallets move reliably without excessive speed. For heavier loads or longer lanes, speed controllers, end stops, lane guides, and entry guides may be needed.
Floor-level pick lanes under or beside storage
Some facilities use floor mounted pallet flow as the pick face below reserve storage or beside a production line. The lane keeps active pallets at floor level while reserve pallets remain in selective rack, bulk storage, or another replenishment area. This can reduce forklift interruptions in the pick zone because replenishment occurs from the loading side while operators pick from the front.
Push-assisted lanes
Some suppliers also describe level, push-assisted floor lanes as part of the floor mounted pallet flow family. These systems may not rely on gravity pitch. Instead, equipment pushes pallets through a controlled lane. This design should be treated carefully. OSHA has addressed unsafe pushing or “bulldozing” practices in powered industrial truck interpretations, so any push-assisted layout should be engineered for that method, supported by defined procedures, and kept separate from improvised pallet pushing in open traffic areas.
Dock and production staging buffers
At docks, floor mounted lanes can separate inbound and outbound flows, organize trailer unloading, or queue loads for shipping waves. In manufacturing, lanes can act as line-side buffers so materials arrive in a known sequence. The system is most effective when staging demand is repeatable. If pallet destinations change constantly, static lanes may become a constraint.
Where floor mounted pallet flow makes sense
The strongest use case is a repeatable flow of similar pallets through a defined process. Good candidates usually share five conditions: predictable SKU movement, a need for FIFO rotation, enough volume to justify dedicated lanes, clear separation between load and pick sides, and pallet loads that remain stable while moving.
Food, beverage, packaging, cold storage, assembly, and distribution operations may consider floor mounted lanes when product age, lot control, or shipment sequence matters. The system is also useful when a team wants to remove loosely staged pallets from aisles and create a visual lane structure without committing to a full rack-supported storage system.
It is not always the right answer. If a facility handles many slow-moving SKUs, highly mixed pallet types, damaged pallets, unstable loads, or frequent priority changes, selective rack or clearly marked floor staging may be more flexible. If the goal is maximum cubic storage, full-height pallet flow rack, drive-in rack, shuttle systems, or other dense storage methods may provide higher capacity than floor-level lanes.
Design questions to answer before specifying lanes
A floor mounted pallet flow project should start with load behavior, not lane hardware. The following questions help determine whether the concept is practical.
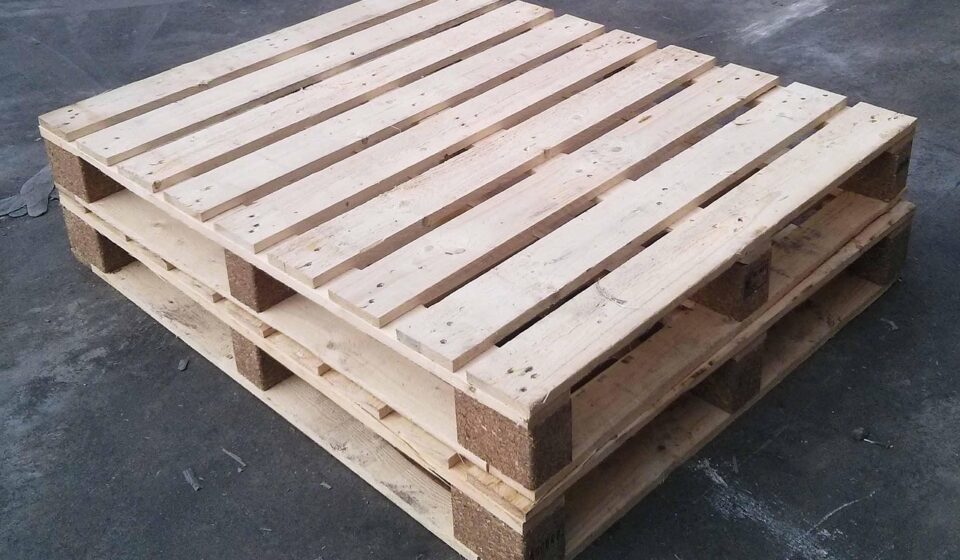
- What pallet types are used? Stringer pallets, block pallets, plastic pallets, export pallets, and damaged wood pallets may behave differently on wheels or rollers.
- What is the load weight range? A lane that works for a narrow weight band may not work safely for a very light load one hour and a very heavy load the next.
- How deep should each lane be? Deeper lanes improve buffering but increase the importance of pallet quality, tracking, speed control, and jam recovery procedures.
- Is true FIFO required? If rotation is critical, the layout should physically separate loading and unloading sides and prevent shortcuts that break sequence.
- What equipment will interact with the lane? Forklifts, walkie pallet trucks, reach trucks, tugger carts, and manual picking all have different clearance and turning needs.
- How will a stuck pallet be recovered? Jam recovery should be planned before installation. Improvised entry into lanes or unsafe lifting practices can turn a storage improvement into a safety problem.
- What condition is the floor in? Floor flatness, slope, cracks, drainage, and freezer heave can affect low-profile flow equipment more than teams expect.
These questions also support supplier comparison. Two layouts that look similar in a drawing may perform differently if one includes braking, entry guides, adequate end stops, and maintenance access while the other is only a basic wheel bed. See also: automation and controls.
Safety and compliance considerations
In the United States, OSHA’s general material handling rule at 29 CFR 1910.176 requires safe clearances where mechanical handling equipment is used, clear and well-maintained aisles, and storage that does not create a hazard. The same rule requires materials stored in tiers to be stable and secure against sliding or collapse. These requirements are directly relevant to any floor mounted pallet flow area because the system concentrates pallets, vehicles, and pedestrians around defined lanes.
Powered industrial truck rules under 29 CFR 1910.178 are also relevant when forklifts, walkie riders, or other powered trucks load and unload the lanes. Operators need training for the actual conditions of use, not only general forklift certification. A narrow staging zone with flowing pallets, end stops, and pedestrian picking activity creates different risks from a wide bulk storage aisle.
For rack-supported designs, ANSI MH16.1-2023 is an important reference because it covers the design, testing, and utilization of industrial steel storage racks, including pallet-flow racks. A purely floor-mounted lane may not have the same structural profile as elevated rack, but any connected rack, overhead reserve storage, or rack-supported pick module should be reviewed under applicable rack standards, local building code requirements, and the equipment supplier’s engineering documentation.
Fire protection and egress should also be checked. Floor mounted lanes can change flue spaces, aisle widths, access to extinguishers, sprinkler clearance assumptions, and emergency travel paths. These issues should be reviewed with qualified safety, fire protection, and code personnel rather than treated as a simple storage rearrangement.
Comparison with other pallet storage choices
| Option | Typical strength | Typical limitation | Best fit |
|---|---|---|---|
| Floor mounted pallet flow | Creates controlled floor-level FIFO lanes and organized staging | Needs consistent pallets, clear procedures, and enough volume for dedicated lanes | Dock buffers, line-side feeding, case picking, cold-room staging |
| Basic floor stacking | Low equipment cost and high flexibility | Rotation control, aisle discipline, and visibility can degrade quickly | Short-term staging or highly variable loads |
| Selective pallet rack | High selectivity and simple access to individual pallets | Lower density than deep-lane systems and more travel aisles | Many SKUs with mixed movement rates |
| Elevated pallet flow rack | High-density FIFO storage using vertical space | Higher structural, installation, and maintenance complexity | Fast-moving products with consistent pallet profiles |
| Push-back rack | Dense storage with a single aisle face | Typically supports last-in, first-out rotation rather than strict FIFO | High-volume inventory where rotation is less time-sensitive |
The practical takeaway is that floor mounted pallet flow is not a universal replacement for racking. It is a process-control tool. It performs well when the facility needs a repeatable movement path at floor level and can define the rules for loading, flow, retrieval, and exception handling.
Implementation checklist
Before installation, warehouse teams should document the operating assumptions that the lane design depends on. A useful checklist includes:
- Approved pallet dimensions, pallet condition rules, and rejected-pallet criteria.
- Minimum and maximum pallet load weights for each lane type.
- Lane depth, lane width, entry side, discharge side, and pick-face protection.
- Required pitch, braking, lane guides, end stops, and impact protection.
- Forklift and pallet truck approach paths, including turning radius and pedestrian separation.
- Jam recovery method that does not require unsafe climbing, lifting, or entry into the lane.
- Inspection schedule for rollers, wheels, anchors, stops, guards, labels, and floor conditions.
- Training for operators, pickers, maintenance staff, and supervisors.
- Change-control rules for new pallet types, heavier loads, lane reconfiguration, or layout changes.
After installation, the first review should focus on real movement rather than drawings. Watch pallets enter, travel, stop, and discharge under normal operating conditions. Look for skewing, hard impacts, unstable loads, blocked aisles, near-miss pedestrian interactions, and shortcuts that break FIFO discipline. Small problems at the start of a lane often become larger maintenance and safety issues after volume increases.
Frequently asked questions
Is floor mounted pallet flow the same as pallet flow rack?
No. Both can support FIFO movement, but standard pallet flow rack is usually built into a rack structure and may use multiple vertical levels. Floor mounted pallet flow places the flow lane at or near floor level, making it more common for staging, picking, and line-side replenishment.
Does every floor mounted system need a slope?
No. Gravity-fed lanes need a controlled pitch so pallets can move forward. Some floor-level systems are push-assisted or use low-profile tracks without relying on gravity. The correct approach depends on pallet weight, lane depth, equipment type, and operating method.
What is the biggest risk with floor mounted pallet flow?
The biggest operational risk is assuming all pallets will behave the same. Damaged pallets, mixed pallet designs, unstable loads, and wide weight variation can cause jams, skewing, hard impacts, or unsafe recovery work. Pallet quality rules are essential.
Can floor mounted pallet flow improve safety?
It can help by organizing pallets into defined lanes and reducing random floor staging, but safety is not automatic. The layout still needs clear aisles, vehicle controls, pedestrian separation, load stability, inspection, and training.
When should a facility avoid it?
A facility should be cautious if SKU movement is unpredictable, pallet quality is poor, loads are unstable, or operators frequently need random access to individual pallets. In those cases, selective rack or flexible marked staging may be more practical.