Glass manufacturing flow chart from raw materials to finished product
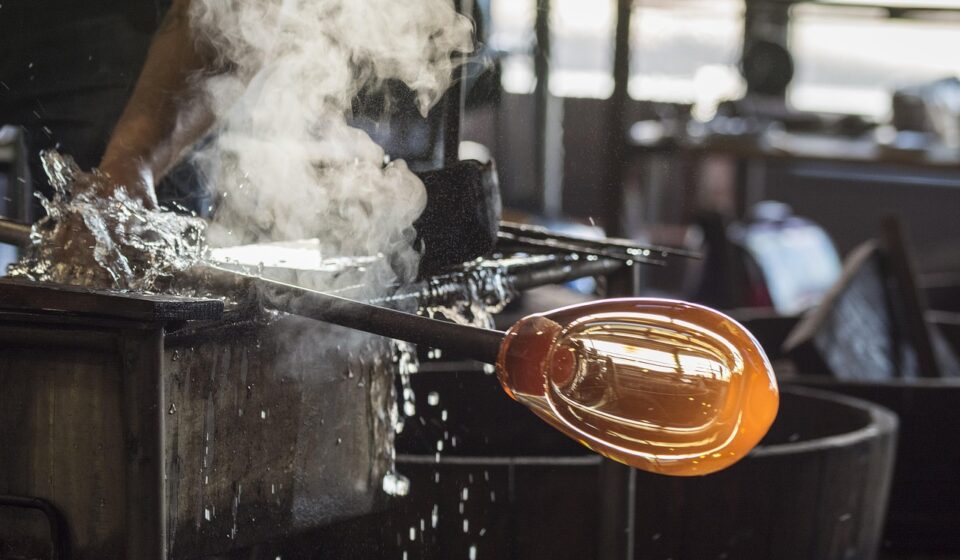
The basic glass manufacturing flow chart
A practical glass manufacturing flow chart begins with raw material storage and ends with inspected, packed product. For most industrial glass, the core sequence is batch preparation, melting and refining, thermal conditioning, forming, annealing, inspection, finishing and packing. The forming step changes by product: float glass flows onto a tin bath, container glass is cut into gobs and formed in molds, and fiberglass is attenuated into fibers. Because melting and refining carry much of the heat demand and quality risk, a useful chart should show more than a straight line. It should also include cullet return, furnace charging, temperature-controlled transfer, reject loops and cold-end inspection.
In simplified form, the flow is:
- Raw material receiving and storage
- Weighing, batching and mixing
- Cullet addition and furnace charging
- Melting, refining and homogenizing
- Conditioning through working end or forehearth
- Product-specific forming
- Annealing in a lehr or controlled cooling zone
- Inspection, cutting, coating, packing or further processing
This sequence is useful for plant planning, operator training, procurement and equipment layout. For more industrial process diagrams and related production-line topics, see the material flow section.
Step-by-step flow for float glass production
Float glass is often the reference case for a glass manufacturing flow chart because the process can be understood as a continuous line. The product is a flat ribbon used as the base for windows, mirrors, automotive glazing, coated glass, laminated glass and many architectural products.
| Stage | Material movement | Typical equipment or control point | Main output |
|---|---|---|---|
| Raw material storage | Silica sand, soda ash, limestone, dolomite, feldspar, additives and cullet are stored separately. | Silos, bins, conveyors, dust collection and material identification systems. | Controlled feedstock inventory. |
| Batching and mixing | Ingredients are weighed to recipe and blended before charging. | Scales, batch mixer, moisture control and batch conveyors. | Uniform mixed batch. |
| Melting and refining | Batch and cullet enter a continuous furnace and become molten glass. | Regenerative, recuperative, oxy-fuel, electric or hybrid melting systems depending on plant design. | Molten glass with reduced unmelted material and fewer bubbles. |
| Conditioning | The melt is thermally adjusted before forming. | Working end, canal and control of temperature, viscosity and flow. | Glass ready for stable ribbon formation. |
| Float bath | Molten glass spreads over molten tin and forms a continuous ribbon. | Controlled atmosphere, top rollers, edge control and ribbon speed control. | Flat glass ribbon with target thickness and surface quality. |
| Annealing lehr | The ribbon is cooled gradually to reduce residual stress. | Temperature zones, rollers, stress monitoring and controlled cooling curve. | Annealed ribbon suitable for cutting and downstream processing. |
| Inspection and cutting | The ribbon passes through online inspection, scoring and snapping. | Optical inspection, defect mapping, edge trimming and automated cutting. | Stock sheets, cut sizes or remelt cullet. |
| Packing or further processing | Accepted sheets are stacked, coated, laminated, tempered or shipped. | Stackers, interleaving systems, coaters, tempering lines and packaging equipment. | Saleable float glass or processed glass. |
Industrial descriptions commonly place the glass melt in the range of about 1300 to 1600°C, depending on composition and furnace design. In float production, public technical references describe glass leaving the melter and entering the float bath at very high temperature, then leaving the bath as a stable ribbon before controlled annealing. Exact temperatures, residence time and furnace arrangement are plant-specific, so a plant-level chart should not copy a generic diagram without checking the actual process data.
How container glass and fiberglass alter the chart
The front end of the chart is similar for many glass products: raw materials are received, weighed, mixed with cullet and melted. The main difference appears at the forming stage, where the same molten material is converted into very different product shapes.
Container glass flow
For bottles and jars, the flow normally changes after the furnace and forehearth. Conditioned glass is delivered to a feeder, sheared into gobs, dropped into molds and formed on individual section machines. A simplified container glass chart is:
- Batching and cullet addition
- Melting and refining in the furnace
- Forehearth temperature conditioning
- Gob forming at the feeder
- Blank mold and final mold forming
- Hot-end surface treatment when required
- Annealing lehr
- Cold-end coating, inspection, rejection, palletizing and packing
Container plants need the flow chart to show reject return and cullet loops clearly. Defective containers from hot-end or cold-end inspection are usually not simple waste. When they are compatible with the batch and uncontaminated, they may return as internal cullet. This loop affects furnace loading, melting behavior and material balance.
Fiberglass flow
Fiberglass production uses a different forming step. After melting and conditioning, the glass may pass through bushings or fiberizing equipment to create fine fibers. Textile fiberglass is drawn into continuous filaments, coated with sizing and wound or chopped. Glass wool for insulation is fiberized, combined with binder, formed into a mat, cured, cut and packaged. In a flow chart, the forming box should not be labeled only as molding or casting. Where relevant, it should identify fiberizing, binder application, curing and density or thickness control.
Key equipment and control points in the line
A strong flow chart is not just a sequence of boxes. It links each stage to the equipment and variables that determine quality, yield and production stability.
- Batch house: Shows storage silos, weighing systems, mixers, conveyors, dust collection and cullet handling. Critical controls include recipe accuracy, moisture, contamination prevention and segregation of glass colors or chemistries.
- Furnace: Converts batch into molten glass. Key variables include pull rate, temperature profile, fuel or electric energy input, refractory condition, combustion control and residence time. Melting is usually the most energy-intensive part of the production line.
- Refining and homogenizing zone: Helps remove bubbles and reduce chemical or thermal non-uniformity. The chart should show this as more than a simple heating step because many defects originate here.
- Working end or forehearth: Conditions the glass to the right temperature and viscosity for forming. Poor control here can cause weight variation in containers, ribbon instability in float glass or diameter variation in fibers.
- Forming equipment: Defines the product. Examples include tin baths for float glass, individual section machines for containers, presses, blow molds, rollers, bushings or fiberizers.
- Annealing lehr: Cools the product under controlled conditions to reduce internal stress. The lehr is not just a cooling tunnel; it is a quality-control stage.
- Inspection and cold end: Includes cameras, dimensional gauges, stress checks, surface inspection, coating, cutting, rejection, stacking and packing.
Where defects, scrap and recycle loops appear
One common gap in simple diagrams is the handling of defects and internal returns. In real production, material flow is not always linear. A practical glass manufacturing flow chart should show where material can be rejected, recycled, reworked or diverted. See also: automation and controls.
| Flow stage | Possible issue | Why it matters | Chart note to include |
|---|---|---|---|
| Raw material receiving | Contaminated sand, incompatible cullet or wrong additive. | Can create stones, color shift or chemistry variation. | Incoming inspection and material segregation. |
| Batching | Wrong weighing, poor mixing or moisture variation. | Can cause non-uniform melting and unstable furnace operation. | Recipe control, batch mixer and moisture checks. |
| Melting and refining | Bubbles, seeds, cords or unmelted particles. | These defects may remain visible or weaken the final product. | Refining zone, residence time and defect monitoring. |
| Forming | Thickness variation, gob weight variation, surface marks or fiber diameter variation. | Product geometry and appearance are set here. | Product-specific forming controls. |
| Annealing | Residual stress from poor cooling. | May increase breakage risk during cutting, handling or use. | Lehr temperature profile and stress inspection. |
| Cutting and packing | Edge chips, scratches, incorrect dimensions or stacking damage. | Good glass can be lost at the cold end. | Inspection gates, reject bins and packing control. |
For flat glass, ASTM C1036 is a useful reference for quality terminology related to annealed flat glass, including blemishes, distortion and dimensional requirements. For heat-strengthened and fully tempered flat glass, ASTM C1048 is commonly used to define requirements after heat treatment. These standards do not replace a plant process chart, but they help align the chart with inspection language and buyer specifications.
How to make the chart useful for engineers and buyers
A chart for general education can remain simple. A chart used for equipment selection, plant audits or procurement needs more detail. The following checks help turn a basic flow into a working industrial document.
- Define the product family first. Do not use a float glass chart for bottles or a container chart for fiberglass. Keep the shared front end, but customize the forming and finishing stages.
- Show the boundary of the process. Clarify whether the chart ends at annealed glass, coated glass, laminated glass, tempered glass, packed containers or finished insulation products.
- Separate primary and secondary processing. Tempering, coating, laminating, insulating glass assembly and mirror backing are often downstream operations, not the basic melting line.
- Mark recycle loops. Internal cullet, rejected sheets, edge trim and broken containers should be shown where they re-enter the process or leave the plant.
- Add control parameters without overloading the chart. Typical items include temperature, pull rate, batch recipe, gob weight, ribbon speed, lehr profile, inspection gates and packing specification.
- Identify quality gates. Place inspection after raw material receiving, after forming, after annealing and before packing. For high-value products, add online and offline inspection separately.
- Include environmental and utility interfaces when needed. Furnace exhaust treatment, dust collection, cooling water, compressed air, combustion air and electric boosting may be important in an engineering flow diagram.
The most accurate glass manufacturing flow chart is product-specific. The common backbone is batching, melting, forming, annealing and inspection, but the industrial value comes from showing where the material changes state, where quality is created, and where losses or returns affect the material balance.
Frequently asked questions
What is the simplest glass manufacturing process flow?
The simplest flow is raw materials and cullet, batching, melting, refining, forming, annealing, inspection and packing. This is suitable for a high-level overview, but it should be customized for float glass, container glass, pressed glass, blown glass or fiberglass.
Where does cullet enter the glass manufacturing flow chart?
Cullet usually enters during batch preparation or just before furnace charging. Internal cullet from the same plant is often easier to control than external cullet because its chemistry and contamination risk are better known. The chart should also show where rejected product becomes cullet again.
Why is annealing included if the glass is already formed?
Annealing reduces internal stress by cooling the glass under controlled conditions. Without proper annealing, the product may look acceptable but become more vulnerable to breakage during cutting, transport, installation or later processing.
Is the float glass process the same as the container glass process?
No. Both share batching and melting, but the forming stage is different. Float glass spreads into a ribbon on molten tin, while container glass is fed as gobs into molds on forming machines. Their inspection, handling and packaging steps also differ.
What should be added to a professional process flow chart?
A professional chart should include equipment names, control points, reject loops, cullet return, inspection gates, utilities and the boundary between primary manufacturing and secondary processing. These additions make the chart useful for engineering, procurement and production troubleshooting.