Metal flow in forging and its role in stronger, cleaner parts
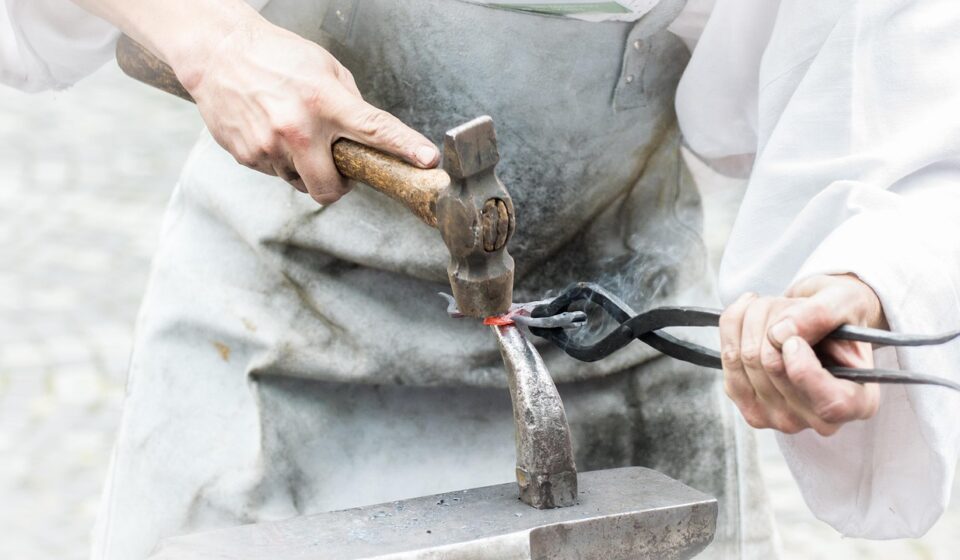
Metal flow in forging is the route a solid billet or preform takes as it plastically deforms under compressive force. It affects whether the die cavity fills completely, whether grain flow follows the expected service load path, and whether defects such as laps, cold shuts, underfill, or internal cracking are likely to form. Good flow is not accidental. It is governed by billet size, temperature, friction, lubrication, die geometry, forging sequence, press or hammer behavior, and the workability of the alloy. For engineers, buyers, and process planners, metal flow is a practical quality issue, not only a metallurgical term.
For related process concepts, see the material flow section.
What metal flow means in forging
Forging deforms metal in the solid state. Unlike casting, where molten metal fills a mold and then solidifies, forging uses pressure to move a billet or preform into a new shape while the material remains solid. The term metal flow describes this movement from one region of the workpiece to another during upsetting, drawing, blocking, finishing, coining, extrusion, or ring rolling.
In practice, engineers look at metal flow at several levels. At the visible level, they check whether material has filled ribs, bosses, flanges, webs, corners, and thin sections. At the tooling level, they study where material is restricted by friction or where it escapes into flash. At the metallurgical level, they consider the resulting grain flow, also called fiber flow or flow lines, which records the deformation path of the material.
Reference works such as ASM Handbook Volume 14A and design materials from the Forging Industry Association discuss grain flow because it can influence directional strength, fatigue behavior, impact resistance, and machining allowances. Grain flow, however, is not a substitute for correct alloy selection, heat treatment, inspection, or process control. It is one part of the wider forging quality system.
Why flow direction matters for forged part quality
The main quality advantage of controlled metal flow is alignment. When a part is forged properly, the internal flow pattern can follow the part shape instead of being cut across critical sections. This matters for components exposed to impact, cyclic load, torsion, bending, or pressure, including gears, rings, shafts, valve bodies, hooks, and structural fittings.
If flow lines bend smoothly around a fillet or along a tooth profile, the part is less likely to contain abrupt internal discontinuities at highly stressed locations. If machining removes too much material or cuts across the flow pattern in a critical zone, part of the benefit of the forging route may be reduced. For this reason, forging design is usually reviewed together with machining stock, parting line location, draft, fillet radius, and final inspection requirements.
Metal flow also affects dimensional quality. A die cavity may look correct in CAD, but if the material cannot reach a thin rib before cooling, the part may show underfill. If two flow fronts meet at a low temperature or fold over each other, a lap or cold shut may remain. If flow is too restricted, forging load rises and the tooling may wear, crack, or deflect earlier than expected.
Key variables that control metal flow
Billet volume and preform shape
The billet must contain enough material to fill the final shape and any required flash. Too little material causes underfill. Too much material can overload tooling, create excessive flash, and increase trimming work. In multi-stage impression forging, the preform can be more important than the final die because it determines where material is available before the finishing blow or press stroke.
Temperature and strain rate
Metals resist deformation differently at different temperatures and forming speeds. Hot forging generally lowers flow stress and improves formability. Cold forging can produce tighter tolerances and good surface finish, but it requires higher loads and careful control of work hardening. Warm forging sits between these conditions. If a workpiece cools too much before the final operation, thin sections and corners become harder to fill and flow-related defects become more likely.
Friction, lubrication, and die surface condition
Friction can help grip the workpiece in some operations, but excessive friction restricts sliding at the die-workpiece interface. That restriction can cause barreling in upsetting, uneven filling in closed dies, higher press loads, and local temperature changes. Lubrication, die coating, scale control, and die surface finish therefore influence both material movement and die life.
Die geometry and parting line
Metal flows toward the path of least resistance. Sharp corners, deep pockets, narrow ribs, abrupt section changes, and poorly placed parting lines make that path harder to manage. Generous fillets, balanced sections, suitable draft, and a logical flash gutter can guide material into the cavity more reliably. Good die design does not simply reproduce the final part shape; it creates a controlled route for the material to reach that shape.
How forging process type changes the flow pattern
Different forging processes provide different levels of flow control. The best choice depends on part geometry, production quantity, alloy, tolerance requirement, and available equipment.
| Forging process | Typical flow behavior | Main quality concern |
|---|---|---|
| Open-die forging | Metal is compressed between simple dies and can flow laterally where it is not constrained. | Maintaining uniform deformation, avoiding centerline defects, and controlling shape through repeated passes. |
| Impression-die forging | Metal is guided into a shaped cavity, often with excess material flowing into flash. | Balancing die fill, flash formation, grain flow, and forging load. |
| Flashless forging | Metal is confined with little or no escape path for excess material. | Accurate billet volume and positioning are critical because extra material has limited space to go. |
| Rolled ring forging | Metal is expanded circumferentially to form seamless rings. | Controlling wall thickness, ring profile, temperature, and circumferential grain flow. |
| Cold extrusion or cold forging | Metal flows through or around tooling at room temperature or near room temperature. | High tooling loads, work hardening, lubrication, and surface integrity. |
Impression-die forging is often associated with the most deliberate flow planning because the cavity, preform, flash land, blocker die, and finisher die must work as a sequence. Open-die forging relies more on operator skill, pass schedule, reduction ratio, rotation, and reheating practice. Both approaches can produce high-integrity parts when the flow path is understood and controlled.
Common defects linked to poor metal flow
Many forging defects have more than one possible cause, but flow behavior is often part of the explanation. The following defects are closely connected to how material moves during deformation.
- Underfill: The die cavity is not completely filled, often at ribs, bosses, corners, or thin extremities. Common contributors include low billet volume, low temperature, high friction, inadequate press energy, or die features that are difficult to fill.
- Laps: A surface fold forms when metal rolls or folds over itself instead of flowing smoothly. Laps can become crack-like discontinuities and may be difficult to remove by machining if they run into the part surface.
- Cold shuts: Two metal fronts meet but do not bond properly. This may happen when flow fronts meet at an unfavorable angle or temperature, or when die design redirects material poorly.
- Internal bursts or chevron cracks: Internal cracking may occur when tensile stress develops within the workpiece during severe deformation, especially in unsuitable process conditions.
- Flow-through or extrusion defects: Material may be forced into an unintended region, creating local thinning, folds, or flash-related problems.
- Excessive flash: Some flash is useful in impression-die forging because it helps build pressure and fill the cavity, but excessive flash wastes material and can indicate poor volume control or die mismatch.
Defect prevention usually requires a combination of design review, process trials, temperature control, lubrication control, equipment capability checks, and inspection. Changing only one variable may not solve the problem if the root cause is the full flow path. See also: automation and controls.
How engineers evaluate and improve metal flow
Metal flow is evaluated before, during, and after production. Before tooling is built, engineers may use experience-based rules, forging design guides, and numerical simulation. Finite element modeling is widely used to estimate die fill, strain, temperature, load, flash formation, and possible fold locations. Simulation does not eliminate trial work, but it helps reduce guesswork and compare design alternatives before expensive tooling changes are made.
During development, short-run trials and cut-up samples can show whether the assumed flow path is realistic. Macroetching can expose flow lines, while dimensional checks show whether the cavity fills consistently. Non-destructive testing may be used when the part duty, specification, or customer requirement calls for surface or internal discontinuity detection.
A practical flow review often asks these questions:
- Does the billet or preform place enough material near the most difficult-to-fill regions?
- Are fillets, radii, ribs, and section transitions suitable for smooth flow?
- Will the parting line and flash land help fill the cavity without overloading the die?
- Is the forging temperature window realistic for the handling time and equipment speed?
- Does lubrication reduce harmful friction without causing surface or environmental problems?
- Will machining allowances preserve important grain flow in critical areas?
- Can inspection methods detect the most likely flow-related defects?
The value comes from connecting these checks rather than treating each defect separately. For example, a lap at a rib may appear to be a local surface issue, but the real cause may be a blocker design that sends material from two directions into a narrow region too late in the stroke. In that case, polishing the die surface may help only slightly, while a preform or die change may be required.
Design implications for industrial buyers and engineers
For buyers, the phrase metal flow should not be treated as a vague marketing claim. It should lead to specific technical questions. Which process is proposed? Where is the parting line? How much machining stock is needed? How are critical sections oriented relative to the expected load? What inspection is specified for laps, folds, cracks, or internal discontinuities? Are there known thin sections or sharp transitions that could create filling problems?
For design engineers, the key lesson is to involve forging process knowledge early. A design that is easy to machine from plate may not be the best forging design, and a compact-looking design may still produce unfavorable flow if the sections are unbalanced. Small changes to radii, wall thickness, rib layout, or machining allowance can make the flow path more reliable without changing the functional purpose of the part.
For production teams, the most useful indicators are consistency and traceability. Stable billet weight, repeatable heating, controlled transfer time, maintained die temperature, verified lubrication, and documented press settings all help keep the actual flow path close to the intended one. When scrap rises, flow-related defects should be analyzed alongside temperature, tooling wear, material lot, equipment condition, and operator practice.
Frequently asked questions
Is metal flow the same as grain flow?
Not exactly. Metal flow describes how the workpiece moves during deformation. Grain flow is the resulting internal pattern left by that deformation. In forging discussions, the terms are related and sometimes used together, but metal flow is the process behavior while grain flow is the metallurgical result.
Does better metal flow always mean a stronger forging?
Better flow can improve die fill, reduce defects, and orient grain flow more favorably. However, strength also depends on alloy chemistry, heat treatment, reduction history, cleanliness, surface condition, and inspection acceptance criteria. A good flow pattern supports quality but does not guarantee performance by itself.
Why does flash help in impression-die forging?
Flash provides an escape path for excess material while also increasing resistance near the end of the stroke. That resistance can help build pressure inside the die cavity and push material into harder-to-fill details. Poor flash design, however, can waste material, raise loads, and shorten die life.
Can simulation fully predict forging defects?
Simulation can identify likely filling problems, strain concentrations, temperature loss, high loads, and possible fold zones. It is most useful when material data, friction assumptions, heat transfer conditions, and equipment behavior are realistic. It should be confirmed with trials, inspection, and production feedback.
What is the simplest way to improve flow in a difficult forging?
There is no single universal fix. Common improvements include adjusting the preform, increasing fillet radii, changing billet volume, improving lubrication, tightening temperature control, revising flash geometry, or changing the forging sequence. The right action depends on where and why the material is failing to flow as intended.