Invent controls and automation for industrial equipment projects
What the phrase means in an industrial project
The search phrase invent controls and automation may refer to a vendor name, but the practical issue for most industrial buyers is broader: how should a team evaluate control panels, PLC logic, variable-speed drives, HMI or SCADA screens, safety functions and cybersecurity before approving an automation upgrade? This article treats the phrase as a procurement and engineering topic, not as a company profile. A sound project starts by defining the control objective, then matching hardware, software, safety, data and lifecycle support to measurable production needs. In 2026, strong automation projects are less about adding more devices and more about connecting reliable control with disciplined OT security, maintainable architecture and operator-friendly diagnostics.
In industrial equipment, controls usually means the hardware and logic that directly command a process: sensors, actuators, PLCs, distributed I/O, VFDs, motor control centers, control panels and safety relays or safety PLCs. Automation is the wider operating system around those controls, including sequences, recipes, alarms, operator interfaces, SCADA, historian data, reporting, remote access and links to maintenance or production systems.
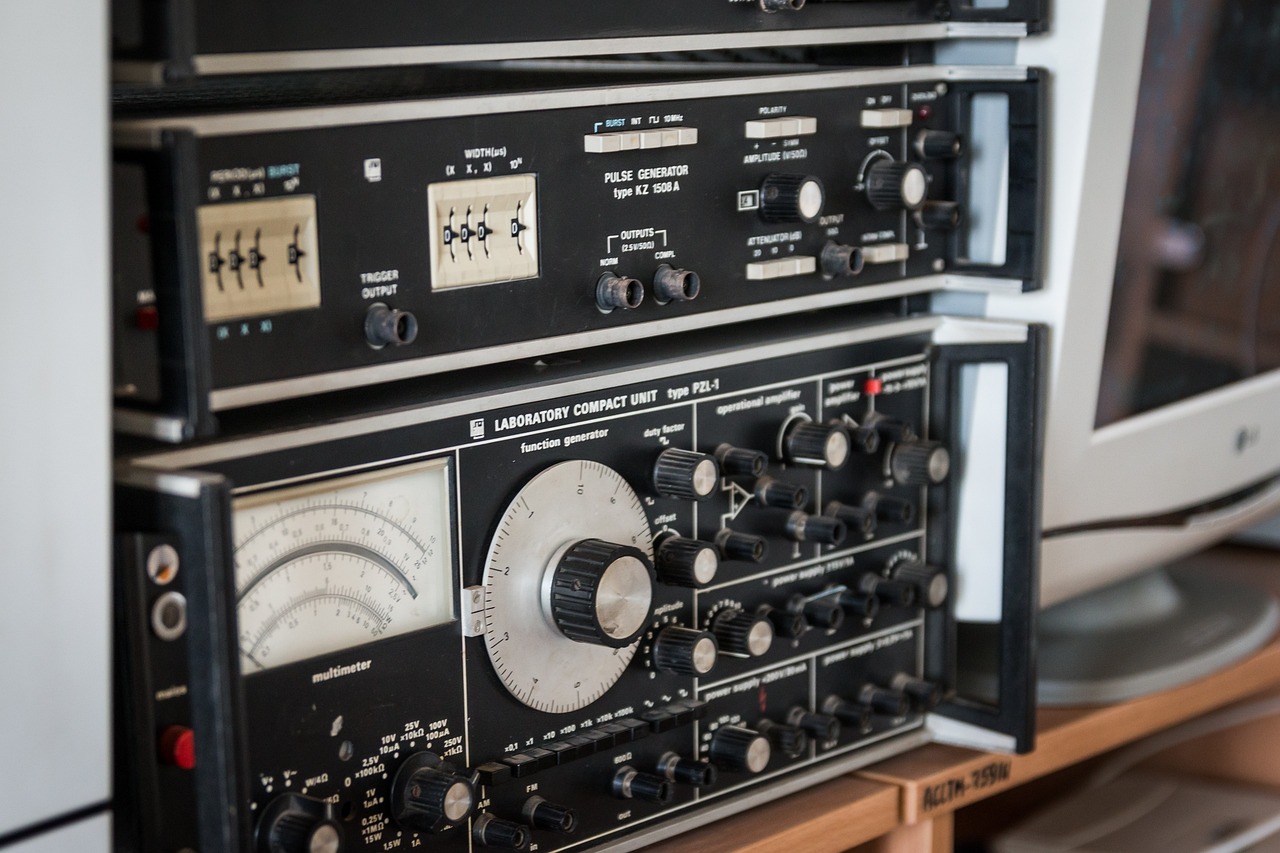
That distinction matters. A machine can have a working panel but still have poor automation if operators cannot diagnose stops, maintenance teams cannot find faults, or management cannot trust production data. The reverse is also common: a plant may have dashboards and cloud tools while the underlying controls remain fragile. For related coverage, see the automation and controls section.
Why controls and automation decisions are changing
Several public industry references point in the same direction: automation is becoming more connected, more data-driven and more security-sensitive. The International Federation of Robotics reported in its World Robotics 2025 material that global industrial robot installations in 2024 were the second-highest annual total on record, exceeding half a million units. Deloitte’s 2026 Manufacturing Industry Outlook reported that, in a 2025 survey of 600 manufacturing executives, 80% planned to invest 20% or more of their improvement budgets in smart manufacturing initiatives, including automation hardware, data analytics, sensors and cloud computing.
Those figures do not mean every factory needs advanced robotics or cloud analytics. They do show that controls projects are no longer isolated electrical upgrades. A PLC replacement, VFD retrofit or HMI modernization can affect production reporting, maintenance planning, network design, cybersecurity controls, spare-parts strategy and operator training. In short, the project boundary has widened.
| Reference point | What it indicates | Project implication |
|---|---|---|
| NIST SP 800-82 Rev. 3, published September 28, 2023 | OT security guidance covers PLCs, DCS, SCADA, network security and risk management. | Security should be designed into control architecture, not added after commissioning. |
| NIST Cybersecurity Framework 2.0, released February 26, 2024 | The framework added Govern to Identify, Protect, Detect, Respond and Recover. | Automation governance, ownership and recovery planning belong in the project scope. |
| ISA/IEC 62443 series | The standards define cybersecurity requirements across the industrial automation and control system lifecycle. | Asset owners, integrators and suppliers need clear responsibility boundaries. |
| IFR World Robotics 2025 | Factory robot adoption remains historically high. | Controls platforms must support safe integration with robotics, vision and motion systems. |
| Deloitte 2026 Manufacturing Industry Outlook | Manufacturers are prioritizing smart manufacturing investment. | Data readiness and workforce capability are now part of automation ROI. |
The core layers of a dependable automation architecture
A practical controls and automation specification should describe system layers, not only list part numbers. This helps buyers compare proposals from panel builders, machine builders and system integrators without letting brand preferences obscure the engineering requirements.
Field and power layer
This layer includes sensors, switches, transmitters, valves, motors, drives, starters, breakers, protection devices and wiring practices. Reliability often starts here. Poor sensor selection, weak grounding, overloaded enclosures or inadequate environmental ratings can make even well-written PLC code unreliable. Specifications should identify operating temperature, dust or moisture exposure, washdown needs, vibration, cable routing, electrical load, short-circuit ratings and maintenance access.
Control and sequence layer
The control layer includes PLCs, PACs, safety controllers, distributed I/O and the program structure that runs the machine or process. Good logic is readable, documented and recoverable. It separates automatic, manual, fault, maintenance and safety states. It also avoids unnecessary customization when standard function blocks or proven libraries are safer to maintain.
Operator and supervisory layer
HMIs and SCADA systems translate control behavior into human decisions. A useful HMI does not simply display every tag. It prioritizes alarms, trends, states, interlocks and recovery steps. Alarm design should reduce nuisance alarms and make abnormal conditions clear. Supervisory systems should also define user roles, audit trails, historian requirements and backup procedures.
Data and integration layer
Modern automation increasingly feeds data to MES, CMMS, quality, energy or enterprise systems. This layer needs careful definition because uncontrolled connectivity can create unreliable data and larger attack surfaces. The specification should state which tags are required, how data is time-stamped, where it is stored, who owns it and what happens when the network connection fails.
Specification checklist before selecting a supplier
Whether a buyer is comparing an automation integrator, a control-panel shop or a named provider found through a search for invent controls and automation, the technical checklist should be the same. The goal is to reduce ambiguity before quotations are compared.
- Process objective: Define the production problem in measurable terms, such as downtime reduction, energy reduction, safer operation, recipe repeatability, throughput stability or data visibility.
- Scope boundary: State what is included and excluded: panel design, PLC programming, HMI screens, field wiring, instrumentation, commissioning, validation, documentation, training and remote support.
- Existing assets: Record current PLC models, drive families, network topology, cabinet drawings, I/O counts, spare parts, firmware versions and known obsolete components.
- Safety requirements: Identify machine guarding, emergency stops, interlocks, safe torque off, lockout procedures and any required safety calculations or validation records.
- Cybersecurity requirements: Define account management, password policy, remote access method, backup approach, patch responsibility, network segmentation and incident recovery expectations.
- Documentation deliverables: Require electrical schematics, I/O lists, tag lists, network diagrams, PLC backups, HMI backups, user manuals and commissioning reports.
- Lifecycle support: Ask how the system will be supported after start-up, including spare parts, software licenses, version control and response procedures.
A lower initial price can become expensive if these items are missing. The most useful proposal is not always the one with the most hardware. It is the one that explains how the control objective will be achieved, tested and maintained.
Cybersecurity and safety are design requirements, not add-ons
Industrial cybersecurity is now part of dependable equipment design because automation systems control physical processes. NIST SP 800-82 Rev. 3, the NIST Cybersecurity Framework 2.0 and the ISA/IEC 62443 series all emphasize risk-based management of operational technology. Their language differs, but the operational message is consistent: know the assets, define responsibilities, protect critical functions, monitor for abnormal activity, and plan recovery before an incident occurs. See also: industrial safety.
For small and mid-sized plants, this does not mean every controls project must become a large security program. It does require basic discipline. Engineering workstations should not be shared without accountability. PLC and HMI backups should be tested, not merely saved. Remote access should be approved, time-limited and logged. Default passwords should be removed. Critical control networks should not be treated like ordinary office networks. Firmware and patch decisions should consider production risk, but deferring every update indefinitely also creates risk.
Safety deserves the same level of attention. A productivity upgrade should never bypass guarding, emergency stops or validated safety functions. If drives, robotics, conveyors or presses are part of the scope, the project should define how safe states are achieved and how restart conditions are controlled. The best automation improves output without making abnormal operation harder to understand.
Where automation creates value and where projects fail
Controls and automation projects usually create value in four ways. First, they reduce unplanned downtime by making faults easier to detect and recover from. Second, they improve repeatability by controlling sequences, recipes, speeds, temperatures, pressures or positions more consistently. Third, they improve energy and asset performance through VFD optimization, load monitoring and better start-stop logic. Fourth, they improve visibility by turning machine signals into trusted production, maintenance and quality data.
Projects fail when the automation scope is treated as a parts purchase rather than an operating change. Common failure points include incomplete site surveys, poor documentation, insufficient operator involvement, weak factory acceptance testing, rushed commissioning, unclear cybersecurity ownership and unrealistic expectations for legacy equipment. Another frequent problem is data without context. A dashboard that reports downtime is useful only if stop reasons, machine states and operator actions are captured consistently.
A practical approach is to separate the project into three decisions: what must be controlled, what must be seen, and what must be preserved. The first decision drives PLC, instrumentation and drive design. The second drives HMI, SCADA and reporting design. The third drives backups, documentation, spares, cybersecurity and training. When these decisions are made together, automation becomes easier to justify and easier to maintain.
Frequently asked questions
Is controls and automation the same as electrical panel building?
No. Panel building is one important part of many controls projects, but automation also includes logic design, operator interfaces, data handling, safety functions, commissioning, documentation and long-term support. A well-built panel can still underperform if the software, network or operating procedure is poorly specified.
What should a buyer ask before approving a PLC or HMI upgrade?
Ask for the current system inventory, the reason for the upgrade, the proposed architecture, the migration plan, the testing plan, the rollback plan and the documentation package. Also ask who owns passwords, backups, software licenses and post-commissioning support.
How should cybersecurity be included in an automation quotation?
Cybersecurity should appear as specific deliverables, not vague wording. Useful items include user-role setup, removal of default passwords, approved remote access, network segmentation notes, backup and restore testing, asset lists and responsibility assignments for patches or firmware updates.
When is a full SCADA system necessary?
SCADA is justified when multiple machines, process areas or utilities need centralized monitoring, alarm management, historian data, reporting or supervisory control. A single standalone machine may only need a well-designed HMI unless plant-wide visibility or compliance reporting is required.
What is the safest way to compare automation suppliers?
Compare suppliers against the same written scope, acceptance criteria and documentation requirements. Brand preference matters less than whether the proposed system is safe, supportable, secure, maintainable and aligned with the production objective.